
Those descriptions identify useful characteristics, but they do not fully identify the mating interface installed on an RRU, RRH or AAU.
For procurement, the connection is better treated as three related specifications:
optical interface → rugged mechanical interface → equipment receptacle
A mismatch at any one of these points can turn an otherwise correct cable into a component that cannot be installed.
This guide focuses specifically on that compatibility problem. For feeder cable, tower closures, fiber counts and complete passive-site architecture, see Glory Optical's 5G FTTA Fiber Optic Solution.
Why an LC-Based FTTA Connector May Not Mate With Another LC-Based Connector
A standard LC connector and a weatherized FTTA connector can share the same optical interface while using different mechanical systems around it.
The distinction is reflected in the standards themselves.
IEC 61754-20 defines the standard interface dimensions of the LC connector family. A separate document, IEC 61754-20-100, addresses LC connectors used inside protective housings and specifies the protective-housing interface separately. The latter standard explicitly describes a protective housing around an internal LC interface.
For an FTTA buyer, this distinction is practical rather than academic.
Consider two assemblies that both contain duplex LC:
- the optical ferrules may be compatible;
- the outer housings may have different diameters;
- the keys may be positioned differently;
- one may use a bayonet lock while another uses a threaded or push-pull system;
- the radio bulkhead may accept only one of them.
The purchase specification therefore has to identify more than the ferrule.
A useful rule is to reserve the word compatible for an assembly whose actual plug has been confirmed against the intended equipment receptacle or an approved mating drawing.
The Three-Layer FTTA Compatibility Model
The following model provides a practical way to review an FTTA cable before it is released for quotation or production.
Optical interface
This layer defines the optical connection carried inside the outdoor system.
Typical fields include:
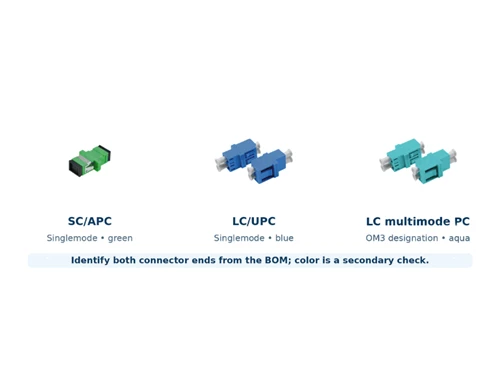
- LC, SC or MPO
- simplex or duplex
- UPC or APC
- single-mode or multimode
- fiber count
- Tx/Rx polarity
TE Connectivity's rugged-fiber documentation illustrates why this layer cannot identify the complete outdoor connector. Its ODVA-style assemblies are available with MPO, LC or SC optical connectors, while its FullAXS assemblies are a separate rugged family using LC connectivity for FTTA applications.
So a purchase description such as "ODVA connector" still needs an optical-interface specification.
Rugged mechanical interface
The second layer covers the parts that allow the connection to survive and operate outdoors:
- connector housing
- key and keyway
- locking method
- plug/socket arrangement
- strain relief
- cable-entry range
- environmental sealing
This is where connector families such as FullAXS, ODVA-style, ODC and Q-ODC need to be distinguished.
HUBER+SUHNER, for example, lists FullAXS, ODC and Q-ODC as separate harsh-environment connector families. FullAXS is described as an FTTA sealing system; ODC uses its own outdoor connector architecture; and Q-ODC adds quick-lock variants with different fiber counts.
Equipment receptacle
The third layer is the actual port installed on the equipment.
For an RFQ, useful evidence can include:
- RRU/RRH/AAU manufacturer
- exact radio model
- port designation
- manufacturer drawing
- clear photographs of the receptacle
- visible key orientation
- existing mating connector part number
This layer should control the final connector decision.
Glory's current FTTA configuration process likewise starts from the radio and optical-module list, checks the port geometry and vendor drawing, and converts that information into an approved interface schedule before the cable BOM is released.
For passive connectivity, the same workflow can be applied to either RRU or AAU projects: the decisive input is the exact equipment receptacle, rather than whether the radio is marketed as an RRU, RRH or AAU.
FullAXS, ODVA and ODC: What Buyers Actually Need to Compare
Connector comparison tables often focus on insertion loss, IP rating and operating temperature. Those values matter after the interface has been identified.
For sourcing, the first comparison should establish the mating architecture.
| Connector Family | Typical Optical Interface | Outdoor Mechanical System | FTTA Procurement Check |
|---|---|---|---|
| FullAXS | Commonly LC-based | Dedicated rugged sealing / mating system | Confirm FullAXS-compatible equipment receptacle |
| ODVA-style | LC, SC or MPO configurations can exist | Weatherized ODVA-style housing | Specify both outer housing and inner optical connector |
| ODC | Family/configuration dependent | Dedicated rugged outdoor connector | Confirm exact ODC plug/socket and equipment side |
| Q-ODC | 2-fiber and higher-count variants exist | Quick-lock outdoor system | Confirm Q-ODC variant, fiber count and mating side |
| PDLC / NSN / other project names | Project dependent | Supplier- or equipment-specific implementation may apply | Request drawing or equipment reference rather than relying on the name alone |
FullAXS should therefore not be treated as another spelling for "waterproof LC," and ODVA should not be treated as one fixed optical ferrule type.
For a confirmed FullAXS equipment interface, Glory offers a FullAXS LC Fiber Patch Cable. Its listed configuration uses two single-mode fibers, LC duplex connectivity, a 4.8 mm cable and a declared maximum insertion loss of 0.30 dB per connector. Product values should still be checked against the final project drawing.
For an ODVA LC application, the ODVA LC Duplex Fiber Optic Patch Cord provides a different outdoor interface and cable construction. Its current listed configuration uses a bayonet locking system and G.657.A2 single-mode fiber.
The two products may both carry LC optical connections, but that fact alone does not establish direct mechanical mating between their outdoor interfaces.
IP67 and IP68 Answer a Different Question From Compatibility
Ingress protection is useful when selecting outdoor equipment, but it is not an interface identification system.
Two connector assemblies can carry the same IP rating and still use incompatible:
- keys;
- housing dimensions;
- mating threads;
- bayonet geometry;
- plug/socket arrangements.
There is also a second procurement issue: the environmental rating may depend on the complete cable-and-connector configuration.
SENKO's IP-RC data sheet provides a useful example. The IP-RC is a weatherproof outer connector system designed around a pre-terminated optical cable. SENKO states that its IP rating was validated with a specified cable and termination procedure and recommends retesting when a different cable type is used. The associated connector kit does not itself contain the fiber optic connector; SENKO recommends an LC uniboot connector inside the rugged housing.
This has two implications for an RFQ.
First, IP67/IP68 should be treated as an environmental requirement, not as evidence that one connector will mate with another.
Second, changing cable OD, jacket construction or termination details can affect the tested sealing configuration.
A better supplier question is therefore:
Which complete mated assembly was ingress-tested, and does the proposed cable construction fall within that tested configuration?
That provides more useful information than an isolated IP value on a datasheet.
Direct Mating and Transition Assemblies Should Not Be Confused
A cross-family cable can connect two different connector systems without making those connector systems directly compatible.
This distinction is particularly important in brownfield upgrades.
HUBER+SUHNER, for example, offers a factory-assembled outdoor cable system with Q-ODC-12 on one side and six FullAXS connections on the other. The product is a pre-assembled transition system; Q-ODC and FullAXS remain separate connector families.
That creates three different procurement situations:
| Situation | Appropriate Interpretation |
|---|---|
| The plug fits the documented equipment receptacle directly | Direct-mate assembly |
| Connector family A is required on one end and family B on the other | Transition cable assembly |
| Compatibility is inferred only from appearance or inner LC | Interface remains unverified |
A transition assembly can be particularly useful when existing outdoor infrastructure remains serviceable but replacement radio equipment uses another interface.
The commercial decision is then no longer "Which connector family should replace everything?"
Instead, the engineer can assess whether a controlled transition between the existing infrastructure and the new equipment avoids unnecessary replacement.
Glory's ODC–FullAXS LC Outdoor Patch Cord follows this concept by putting different rugged interfaces at opposite ends of one assembly. The exact ODC and FullAXS mating requirements should be confirmed against the project drawing before use.
A Better RFQ Starts With Interface Evidence
For a repeat rollout, a supplier should receive enough information to reproduce the same approved interface without guessing from product photographs.
The following table can be used as the commercial release sheet.
| RFQ Field | What to Provide | Why It Matters |
|---|---|---|
| Radio / equipment | Manufacturer, exact RRU/RRH/AAU model | Identifies the equipment family |
| Receptacle evidence | Port drawing, photos, port number, existing mating P/N | Confirms housing geometry and keying |
| Rugged connector | FullAXS, ODVA, ODC or approved project designation | Defines the external mating system |
| Optical interface | LC/SC/MPO, UPC/APC, fiber count, polarity | Defines optical mating |
| Cable construction | Fiber type, cable OD, jacket, armor, length | Controls strain relief, routing and sealing |
| Environment | Required mated-state IP rating, temperature, UV/exposure conditions | Defines environmental qualification |
| Acceptance evidence | IL/RL report, end-face inspection, polarity, label/serial format | Defines production acceptance |
| Approval route | Drawing approval, sample quantity, mating test, production release | Prevents an assumption becoming a bulk-order error |
The most important row is often receptacle evidence.
A clear photo is useful, but it should preferably be paired with the radio model or port drawing. Connector housings from different families can be visually similar enough that a photograph alone may not be a safe procurement specification.
From RFQ to Volume Production: Where Sample Approval Adds Value
Connector compatibility is one of the FTTA characteristics that is difficult to recover from after a bulk order has already been manufactured.
For project-specific cable assemblies, Glory's published FTTA configuration method uses the radio model and port drawing to confirm the interface, followed by sample and test-field approval before volume production when the assembly is project-specific.
That workflow creates a useful separation between specification approval and production release.
A practical approval sequence can look like this:
Radio model, receptacle evidence, cable length, cable construction and required test format are submitted with the RFQ.
The quotation is tied to a controlled drawing or configuration sheet showing both connector ends, cable OD, length and critical mating details.
A pre-production assembly is made against the approved configuration.
The sample is connected to the actual equipment receptacle or an approved reference interface.
Insertion loss, return loss where specified, polarity and end-face condition are checked against the project's acceptance criteria.
The approved sample/configuration becomes the production reference.
This approach is especially valuable for connector names that are used inconsistently between suppliers or equipment generations.
It also gives purchasing teams something more concrete than a statement such as "compatible with Brand X radios."
For project-specific interfaces, use Glory's custom FTTA cable assembly route rather than assuming that a catalogue connector name covers every radio in the same vendor family. Glory's solution page explicitly treats product-page specifications as listed configurations and the approved project drawing as the controlling production reference.
Optical Acceptance Still Matters After Mechanical Compatibility Is Confirmed
Mechanical mating answers whether the cable can be connected. It does not confirm the quality of the optical path.
Connector end faces should be inspected and optical performance should be measured against the agreed project specification.
IEC 61300-3-35 provides the industry framework for visual inspection of fiber optic connector and transceiver end faces. This is particularly relevant when assemblies have been repeatedly handled during sample mating, installation or commissioning.
For procurement purposes, the production record can include:
- assembly identification or serial number;
- actual insertion-loss result;
- return-loss result when required;
- polarity/continuity result;
- end-face inspection status;
- cable length;
- project/site label.
Glory's current ODC–FullAXS product page states that units are tested before shipment and lists IL/RL values for its standard configuration, while Glory's broader FTTA solution describes per-pair optical test documentation for pre-terminated assemblies.
The acceptance limit itself should come from the approved project specification rather than being copied from a generic online guide.
Which Glory FTTA Cable Assembly Fits Which Procurement Situation?
The connector should follow the approved mating interface. The following recommendations use products currently listed in Glory Optical's Fiber Optic Cable Assemblies range. Select by the actual equipment receptacle and approved project drawing, not by connector appearance alone.


FTTA Connector Compatibility FAQs
Q: Can two FTTA cables both use LC and still be incompatible?
A: Yes. LC may describe the optical connection inside the assembly, while the external rugged housing, keying and locking system are different. Direct compatibility should be confirmed at the complete plug-and-receptacle level.
Q: What information is most useful for identifying an RRU fiber connector?
A: The exact RRU/RRH/AAU model plus the equipment port drawing is the strongest starting point. Clear photographs, key orientation and an existing mating-part number can provide additional confirmation.
Q: Are FullAXS and ODVA directly interchangeable?
A: They should be treated as different rugged connector systems unless the equipment or connector manufacturer documents a direct mating interface. Both may use LC internally without sharing the same outer mechanical interface.
Q: Does an IP68 rating mean two outdoor fiber connectors are compatible?
A: No. An IP rating describes ingress protection under the tested configuration. It does not define connector geometry, keying or mating architecture.
Q: What is the difference between direct compatibility and a transition cable?
A: Direct compatibility means the connector plug mates with the required receptacle. A transition cable deliberately uses one connector family at one end and another at the opposite end to connect two different interfaces.
Q: When should a buyer request an FTTA sample before bulk production?
A: Sample approval is particularly useful when the connector name is ambiguous, the equipment generation is uncertain, a new cable OD or housing is being used, or the project requires a custom transition between two connector families.
Final Procurement Decision
For an FTTA cable, the connector name is only one field in the specification.
The release decision should be traceable through:
equipment receptacle → rugged mating interface → optical interface → cable construction → approved sample/test evidence
Following that path makes it much easier to distinguish a genuinely compatible cable from one that merely has the right fiber count, the right LC ferrules and a similar-looking waterproof housing.
For a single standard interface, select the corresponding factory-terminated cable assembly.
For mixed or uncertain interfaces, provide the radio model, port drawing and required cable construction before the quotation is finalized. That gives the supplier enough information to confirm the mating arrangement and, where necessary, move through sample approval before volume production.